
Maximizing Safety And Efficiency: The Backbone Of Drug Storage Systems
By Tom Seest
At RackingWorld, we help guide you through selecting warehouse storage systems and racking.
Be sure to read our other related stories at RackingWorld to learn more about warehouse storage systems.
How Do Drug Manufacturing Facilities Leverage Pallet Racking?
In drug manufacturing facilities, pallet racking isn’t just about stacking boxes—it’s the backbone that keeps everything running smooth, safe, and on time. Think about it: these places juggle hundreds of different materials, from raw ingredients to finished products, all needing tight control. Without a solid pallet racking system, chaos would take over fast—mix-ups happen, delays pile up, and worst of all, safety can slip through the cracks.
On the floor, pallet racking turns clutter into order. It’s like the silent workhorse that keeps crews moving, loading and unloading without a second thought. When you’ve got racks arranged right, you’re cutting down wasted steps and time, which means your team can focus on the real job: making life-saving medicine. And that’s a big deal. Every box sitting on those racks carries the weight of responsibility—not just for the product, but for the people who depend on it. When you see a row of neat, sturdy pallet racking, it’s a sign the place respects both its mission and its workforce.
There’s a certain pride in knowing the pallet racking setup is solid—engineered strong enough to handle the heavy loads, designed smart enough to fit in tight quarters, but flexible enough to adapt as needs change. That’s practical know-how born from years of getting it wrong and fixing it right. You don’t wing it here; precision and reliability mean everything when you’re working with materials that have strict regulations and expiration dates. Pallet racking helps ensure everything stays where it should, traceable and accounted for, cutting down on costly mistakes or recalls.
More than just shelves or metal beams, pallet racking in drug manufacturing facilities builds trust—between the company, regulators, and, most importantly, the patients waiting on those medicines. It ties the whole chain together, making sure every part of that process stands up to scrutiny. When you see a rack full of organized, easy-to-access pallets, you’re looking at a silent promise that the job’s being done right.
Bottom line: pallet racking isn’t glamorous, but it’s essential. It’s the kind of no-nonsense solution you lean on when lives are on the line and deadlines don’t budge. It keeps a facility not just functioning, but thriving, with all hands on deck confident their work rests on a foundation built to last.

How Do Drug Manufacturing Facilities Leverage Pallet Racking?
How Do Drug Manufacturing Facilities Leverage Pallet Racking?
- Pallet racking is essential in drug manufacturing for organizing hundreds of materials, ensuring smooth, safe, and timely operations.
- It transforms clutter into order, enabling efficient movement, loading, and unloading, reducing wasted time and steps.
- Proper pallet racking supports the critical mission of producing life-saving medicines by maintaining responsibility for products and people.
- The system is engineered for strength, smart design, and flexibility to meet strict regulations and adapt to changing needs.
- It ensures materials remain traceable and accounted for, minimizing costly errors and recalls.
- Pallet racking builds trust among companies, regulators, and patients by upholding rigorous standards throughout the supply chain.
- Though not glamorous, pallet racking is a reliable, no-nonsense foundation that keeps drug manufacturing facilities functioning effectively and confidently.

How Do Drug Manufacturing Facilities Leverage Pallet Racking?
Table Of Contents
- How Do Drug Manufacturing Facilities Leverage Pallet Racking?
- How Does Pallet Racking Improve Drug Storage Efficiency?
- How Can Pallet Racking Enhance Product Safety In Pharma?
- What Role Does Pallet Racking Play In Quality Control?
- How Does Pallet Racking Support Regulatory Compliance?
- Can Pallet Racking Reduce Contamination Risks?
- How Does Optimized Pallet Racking Save Operational Costs?
- Conclusion
- Other Resources
- Glossary Of Terms
- Other Questions
- Checklist
How Does Pallet Racking Improve Drug Storage Efficiency?
When it comes to storing drugs, every inch of space counts and every minute matters. Pallet racking steps in like a trusty workhorse, turning cramped, cluttered storage rooms into well-oiled machines. You don’t just get more shelf space—you get a whole new way of working smarter, not harder. Picture this: instead of digging through piles or stacking boxes precariously, everything is easy to find, easy to reach, and safely organized. That kind of order doesn’t just save time, it saves lives.
There’s a real peace of mind knowing your inventory is tight, tracked, and tidy. Pallet racking systems give you the confidence that the right drug is exactly where you expect it when the clock’s ticking. No fumbling around in a mess, no stress about damaged or expired stock hidden in the back. The workday becomes less guesswork and more get-to-it, which matters when you’re dealing with medicine that people rely on.
Ethically, it’s about doing your job right, respecting the responsibility that comes with handling drugs. Pallet racking helps keep things clean, safe, and compliant with regulations—because shortcuts here aren’t just costly, they’re dangerous. When storage meets real-world demands through a solid racking system, you’re stepping up your game in a way that protects both your team and the patients depending on you.
There’s something about seeing a well-set-up warehouse that speaks to hands-on experience. It’s a story of problem-solving, grit, and knowing that when the pressure’s on, you can count on your gear. If you’ve ever wrestled with bottlenecks or stockpile chaos, pallet racking offers a straightforward fix—fitting perfectly with the no-nonsense, show-up-and-get-it-done attitude at the heart of good drug storage.
On a bigger level, pallet racking boosts efficiency not just for one person or one day, but for every team member and every shift down the line. It’s a silent partner in the shared goal of getting urgently needed medicine out the door without a hitch. Trust in a system that’s built tough, down-to-earth, and steady—because when it comes to drug storage, efficiency isn’t just a buzzword, it’s the backbone of a safer, smoother operation.

How Does Pallet Racking Improve Drug Storage Efficiency?
How Does Pallet Racking Improve Drug Storage Efficiency?
- Pallet racking optimizes limited storage space and time, transforming cluttered rooms into efficient, organized areas.
- It enables easier access, better organization, and safer handling of drugs, reducing time spent searching and minimizing risks.
- Inventory becomes tightly tracked and tidy, ensuring the right drug is available precisely when needed.
- Pallet racking supports ethical handling by maintaining cleanliness, safety, and regulatory compliance, preventing costly and dangerous shortcuts.
- A well-organized storage system reflects hands-on experience, problem-solving, and reliability under pressure.
- It resolves common storage issues like bottlenecks and stockpile chaos, aligning with a practical, efficient work approach.
- The system enhances efficiency not only for individual workers but across all shifts, supporting timely delivery of critical medicine.
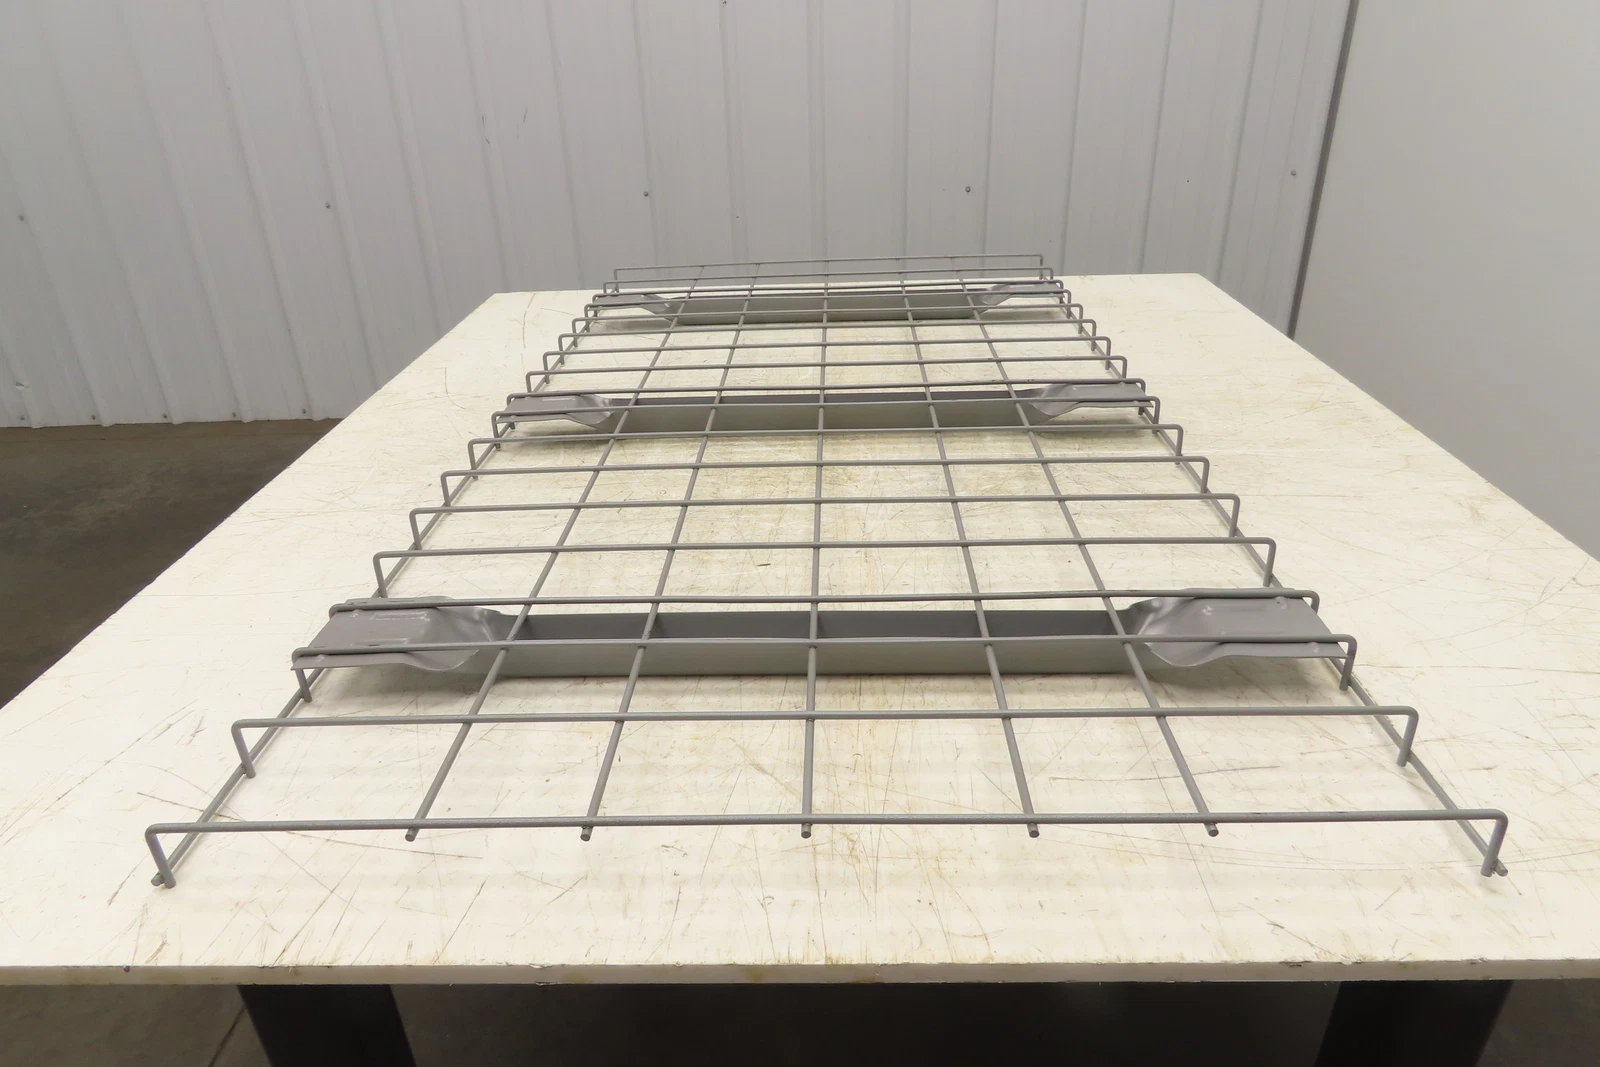
How Does Pallet Racking Improve Drug Storage Efficiency?
How Can Pallet Racking Enhance Product Safety In Pharma?
When it comes to keeping pharma products safe, pallet racking isn’t just a fancy shelf—it’s the backbone that stands between your carefully made medicines and a costly, messy disaster. Think about the value packed into every box: months of research, sweat, and hope poured into cures that people depend on. You can’t just toss those pallets onto the floor and hope for the best. Pallet racking steps in like a steady pair of hands, organizing, protecting, and securing those precious goods in a way that respects their worth.
From the ground up, pallet racking keeps things off the floor, away from dirt, moisture, and accidental run-ins by forklifts or workers. It’s the practical, no-frills solution that takes the chaos of a busy warehouse and turns it into a system where every product has its place. That order doesn’t just prevent damage—it saves lives. After all, in pharmaceuticals, a broken vial or contaminated batch isn’t just a loss off the books. It’s a risk to patients, a hit to trust, and a shadow over everyone’s conscience.
On the ethical side, knowing your pallet racking holds fast means you’re doing right by the folks who depend on those medicines. You’re honoring the integrity of the entire supply chain, standing guard in a silent but powerful way. It’s about knowing you’ve built a fortress, not just stacked boxes. That’s a responsibility every warehouse team shoulders with grit and care, and pallet racking is the tool that lets you carry that weight without breaking a sweat.
Experience shows that when pallet racking is sound, inspections go smoother, turnover is faster, and everyone—from managers to forklift drivers—feels confident in handling what’s truly valuable. It encourages a culture where safety isn’t just a checklist but a shared mission. That makes a difference you can see in the smooth hum of daily operations and in the pride workers carry knowing they play a part in something bigger than themselves.
So, investing in quality pallet racking is investing in peace of mind. It’s about more than cubicles and forklifts; it’s about respect for the work behind every product, for the people who rely on them, and for the honest, hands-on folks who keep the world running. Don’t just stack your goods—stand behind them with pallet racking that holds the line.

How Can Pallet Racking Enhance Product Safety In Pharma?
How Can Pallet Racking Enhance Product Safety In Pharma?
- Pallet racking is essential for protecting pharmaceutical products, safeguarding valuable medicines from damage and contamination.
- It keeps products off the floor, protecting them from dirt, moisture, and accidents with forklifts or workers.
- Pallet racking organizes warehouse inventory, creating order that prevents damage and supports patient safety.
- It upholds the ethical responsibility of maintaining the integrity of the pharmaceutical supply chain.
- Reliable pallet racking improves inspection efficiency, speeds up turnover, and boosts confidence among warehouse staff.
- It fosters a safety culture where protection of valuable goods is a shared mission, enhancing operational smoothness and worker pride.
- Investing in quality pallet racking equates to respecting the value of the products, the people who depend on them, and the workforce maintaining the supply chain.
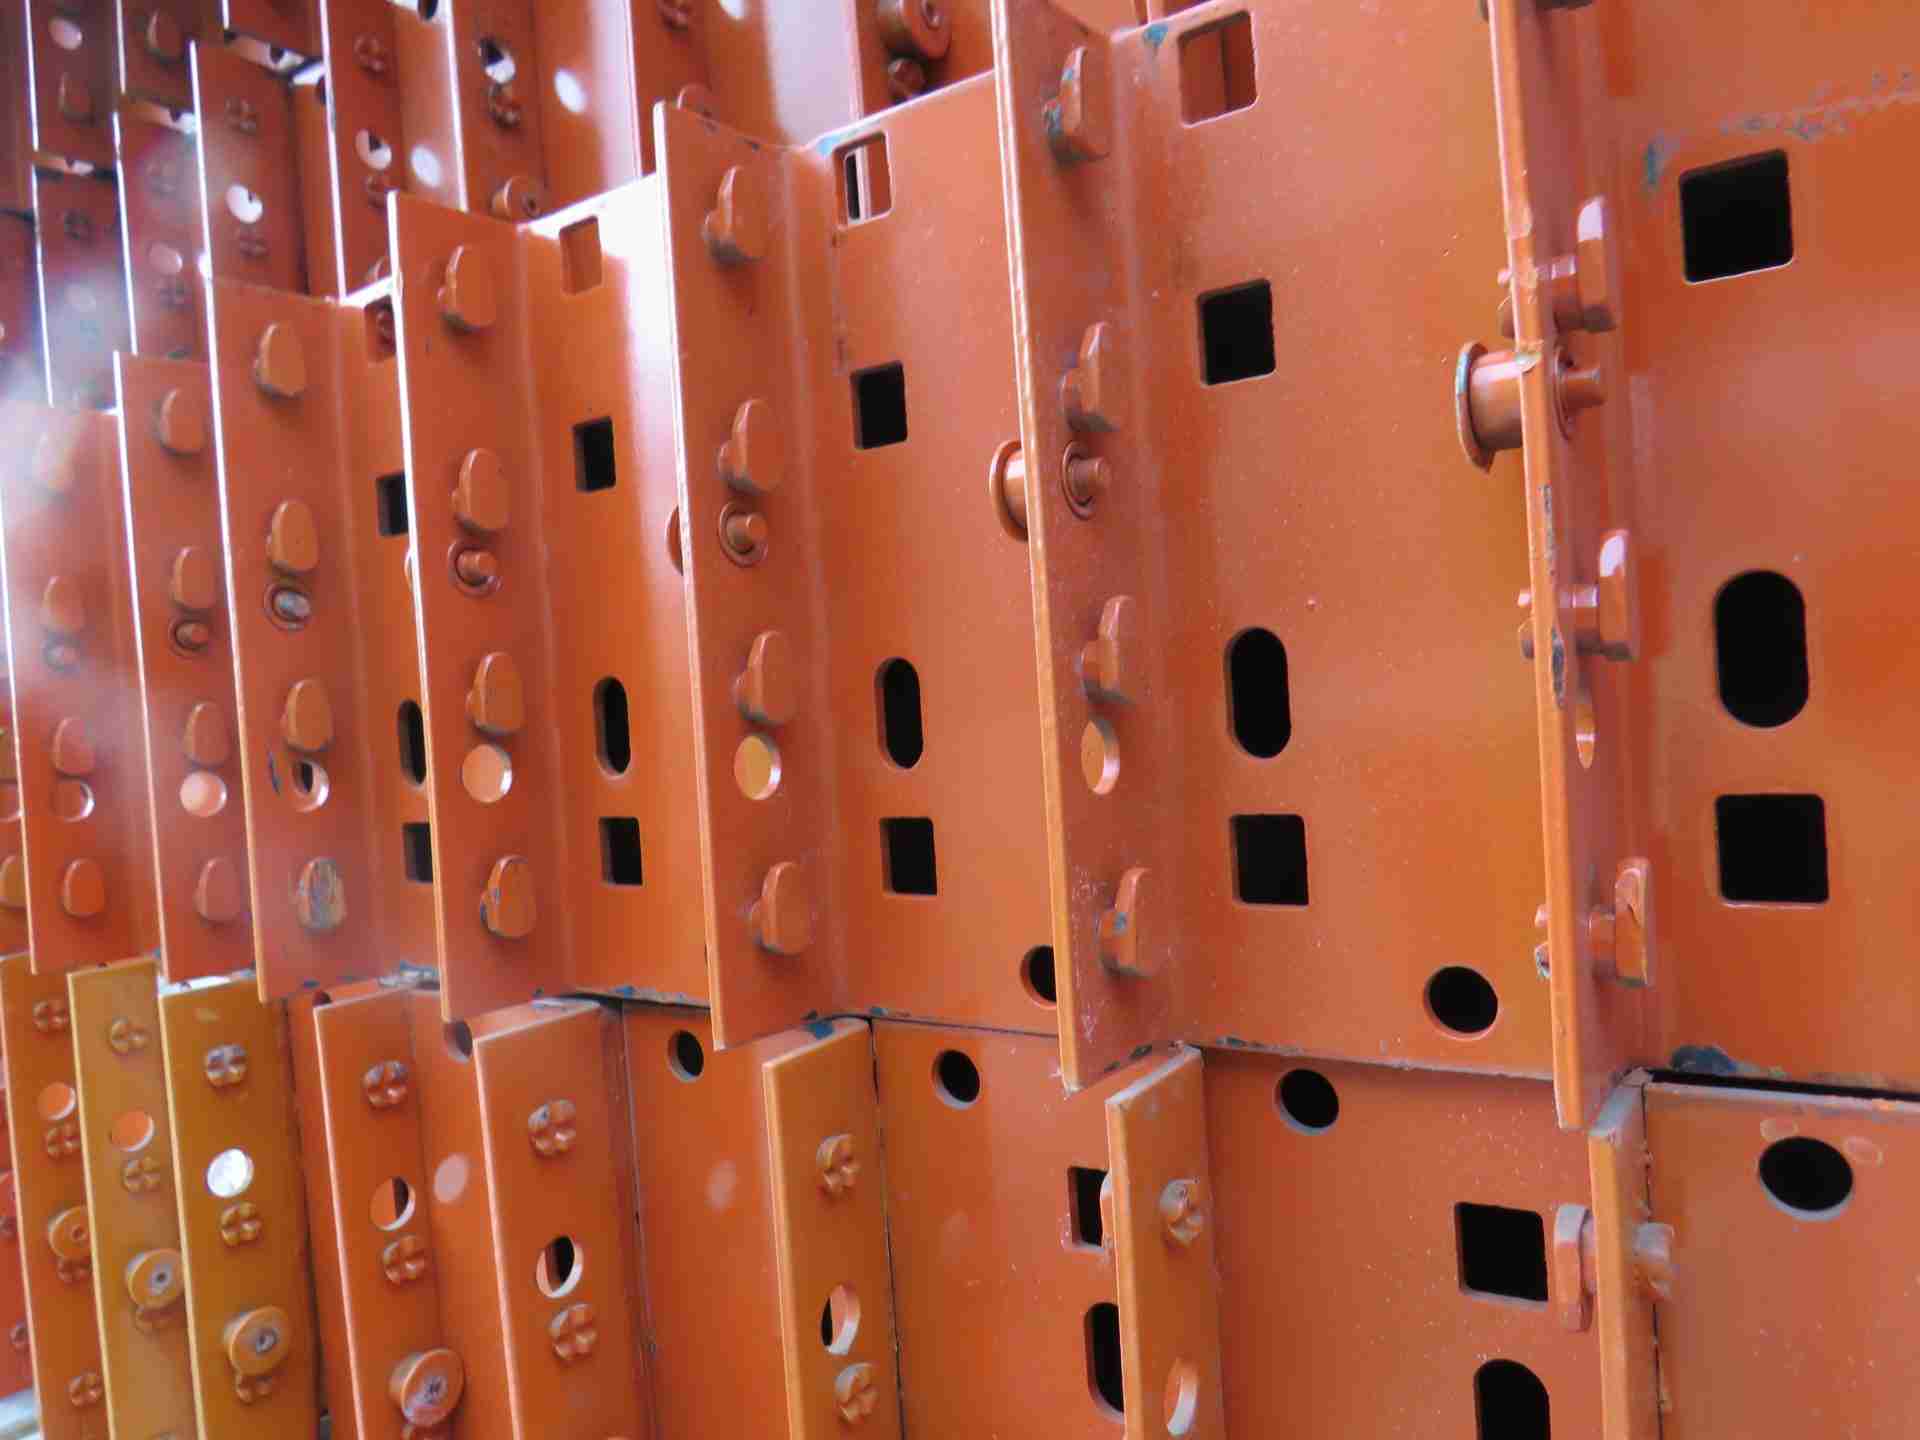
How Can Pallet Racking Enhance Product Safety In Pharma?
What Role Does Pallet Racking Play In Quality Control?
You don’t often hear folks singing praises about pallet racking like it’s the star of the show, but here’s the truth: pallet racking ain’t just a stack-it-up-and-forget-it kind of thing. It’s the backbone of keeping things right, proper, and running smooth out there on the floor. When you’ve spent time in warehouses, loading docks, or on distribution lines, you know that a sloppy setup isn’t just an eyesore—it’s a quality control nightmare waiting to happen.
Think about it. Pallet racking holds everything steady, giving each product its own place, almost like a well-made tool belt. When stuff is properly stored, it’s less likely to get banged up, crushed, or mixed up with something it shouldn’t be. That’s a big deal because damage or confusion in stock spills over directly to the customer. Nobody wants to receive a busted part or a wrong order—those aren’t just mistakes; they’re trust lost. The right pallet racking system keeps you honest and organized, and that’s a promise you make to the people counting on you.
Let’s be straight: no amount of fancy packaging or slick branding can fix a warehouse that’s a mess. A quality pallet racking setup brings a certain integrity. It’s not just metal bars bolted to the floor; it’s the quiet enforcer of good habits. It says, “We value these goods, we respect the process, and we care about what happens from our hands to yours.” That’s the kind of message that sticks with customers and workers alike. It makes everyone feel part of something done right.
On the practical side, pallet racking saves time and reduces costly errors. When goods are easy to find and access, audits, inspections, and inventory management are cleaner and quicker. That efficiency doesn’t just save dollars—it saves headaches and builds confidence. It shows up in fewer returns, less waste, and a smoother workflow. That’s not just good business sense; it’s how you honor the hard work behind every product.
Pallet racking isn’t just storage; it’s a silent partner in quality control. It holds more than pallets—it holds your standards, your reputation, and your commitment to doing things the right way, every time. When you’ve got the right pallet racking in place, you’re not just stacking goods—you’re stacking trust.

What Role Does Pallet Racking Play In Quality Control?
What Role Does Pallet Racking Play In Quality Control?
- Pallet racking is essential for maintaining order and efficiency in warehouses, loading docks, and distribution lines, preventing quality control issues.
- It securely holds products in place, reducing damage, crushing, and mix-ups that can harm customer trust.
- A proper pallet racking system reflects organizational integrity and respect for the goods and processes involved.
- It enforces good habits and communicates care from the warehouse to the customer, benefiting both workers and clients.
- Pallet racking improves practical operations by saving time, reducing errors, and streamlining audits, inspections, and inventory management.
- Efficiency gains from pallet racking lead to fewer returns, less waste, and smoother workflows, supporting overall business success.
- Beyond storage, pallet racking upholds standards, reputation, and commitment to quality, effectively stacking trust along with goods.
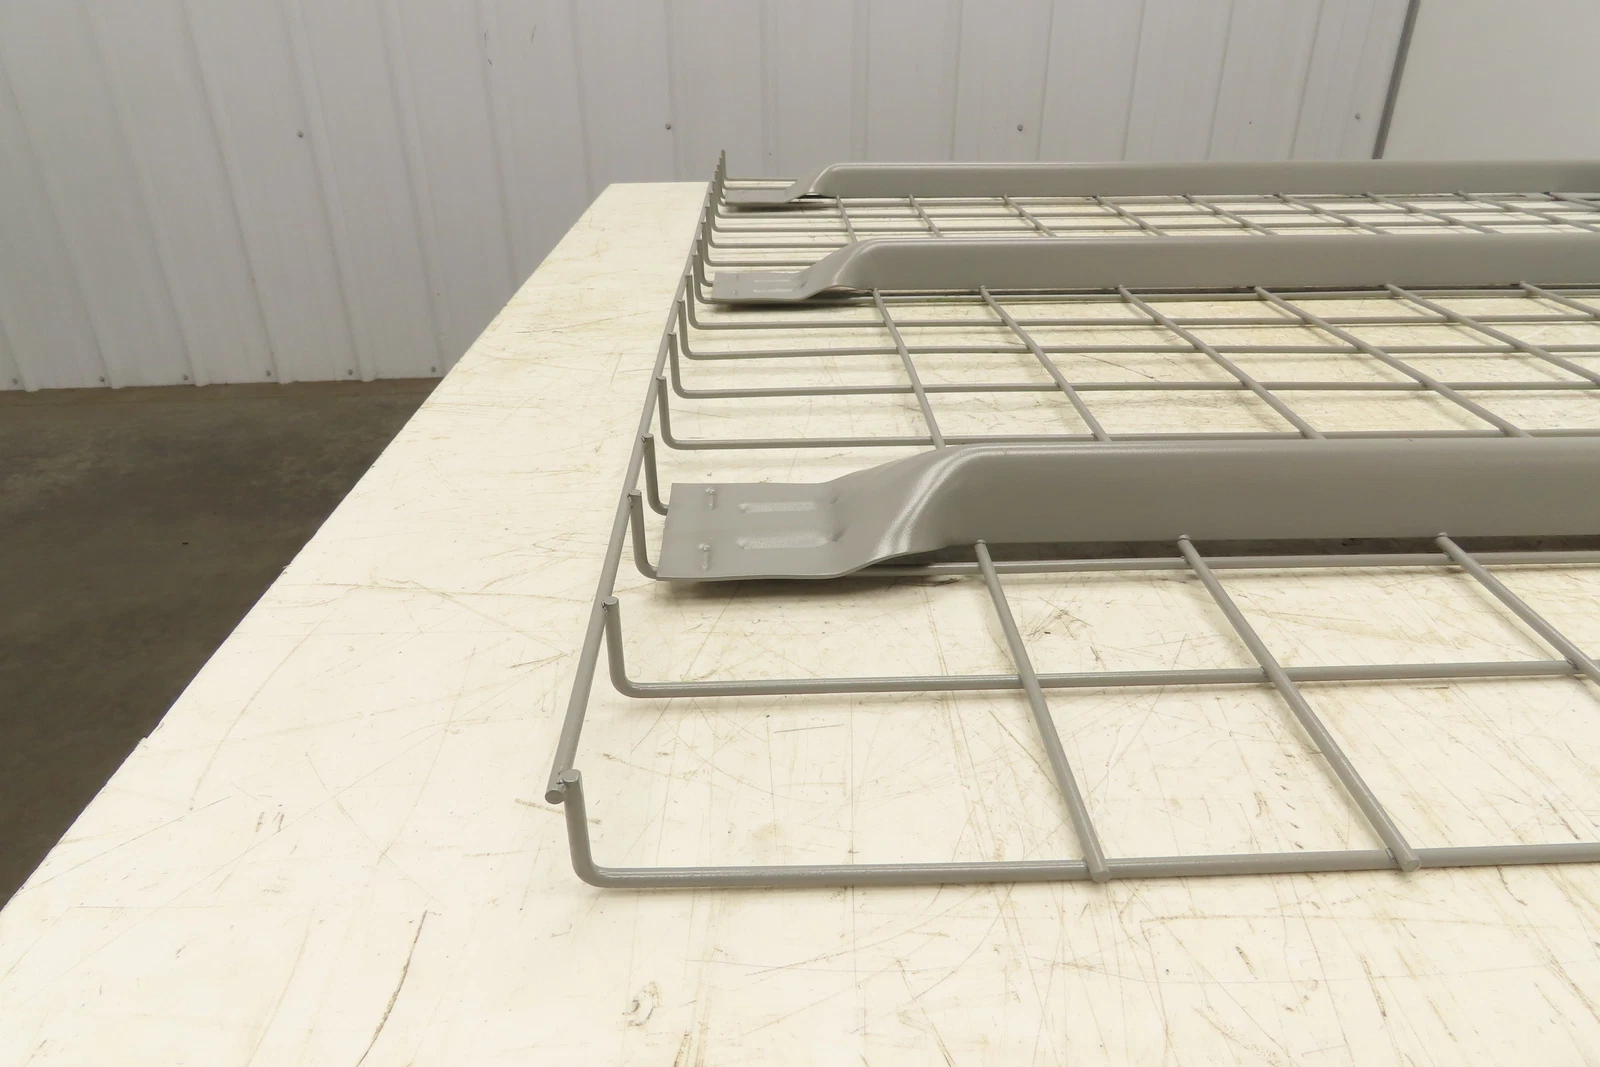
What Role Does Pallet Racking Play In Quality Control?
How Does Pallet Racking Support Regulatory Compliance?
When you’re out there day in and day out stacking pallets, moving heavy loads, and fitting everything just right on racks, you’re not just juggling space—you’re juggling safety, legality, and peace of mind. Pallet racking isn’t fancy or flashy, but it’s the backbone of getting your warehouse or storage area humming without worry. It’s what keeps the inspectors nodding, the insurance folks from twitching, and your crew walking through the door each morning knowing they’re not risking life and limb. That’s regulatory compliance in action, plain and simple.
You see, pallet racking systems are designed with rules in mind—rules laid down by folks who have spent their lives trying to prevent accidents, fires, and expensive mishaps. Those regulations may sound like red tape, but they exist because someone paid the price the hard way. Properly installed and maintained pallet racking meets fire codes, weight limits, and spacing guidelines that keep your goods and your people safe. Put anything less in place, and you’re inviting trouble big enough to sink a business, not to mention the harm it can do to folks depending on you.
There’s a strong ethical thread here, too. Knowing that your racking system supports compliance means you’re doing right by everyone helping you put food on the table, by your customers counting on you to deliver, and by the wider community that trusts you’ll keep it all running safe and sound. It’s a responsible way to run a business—no cutting corners or hoping for the best. When your pallet racking is up to snuff, you’re literally raising the bar for safety and reliability.
From a practical standpoint, compliance saves you money and time. Avoiding fines, dodging shutdown orders, and preventing costly damage to goods all boil down to smart pallet racking choices. Just ask anyone who’s dealt with the headache of an unexpected inspection or a collapsed shelf. That gut punch can be avoided by sticking to proven setups that meet or exceed guidelines.
At the end of the day, pallet racking is more than metal beams and boards—it’s a statement that you take your work seriously, respect your people, and have the foresight to keep everything running smooth and safe. Investing in the right pallet racking systems invites trust—among employees, inspectors, and business partners alike—and that trust is worth its weight in gold. Make compliance a cornerstone, and you’re not just following rules; you’re building a foundation that holds your entire operation upright.

How Does Pallet Racking Support Regulatory Compliance?
How Does Pallet Racking Support Regulatory Compliance?
- Pallet racking is essential for safety, legality, and operational peace of mind in warehouses and storage areas.
- Systems are designed to meet strict regulations aimed at preventing accidents, fires, and costly damages.
- Compliance with fire codes, weight limits, and spacing guidelines protects both goods and personnel.
- Ethical responsibility underpins compliance, ensuring safety for workers, customers, and the wider community.
- Proper pallet racking prevents fines, shutdowns, and damages, saving money and time.
- Choosing compliant setups avoids the risks and disruptions caused by unexpected inspections or failures.
- Investing in the right pallet racking builds trust among employees, inspectors, and partners while supporting reliable operations.
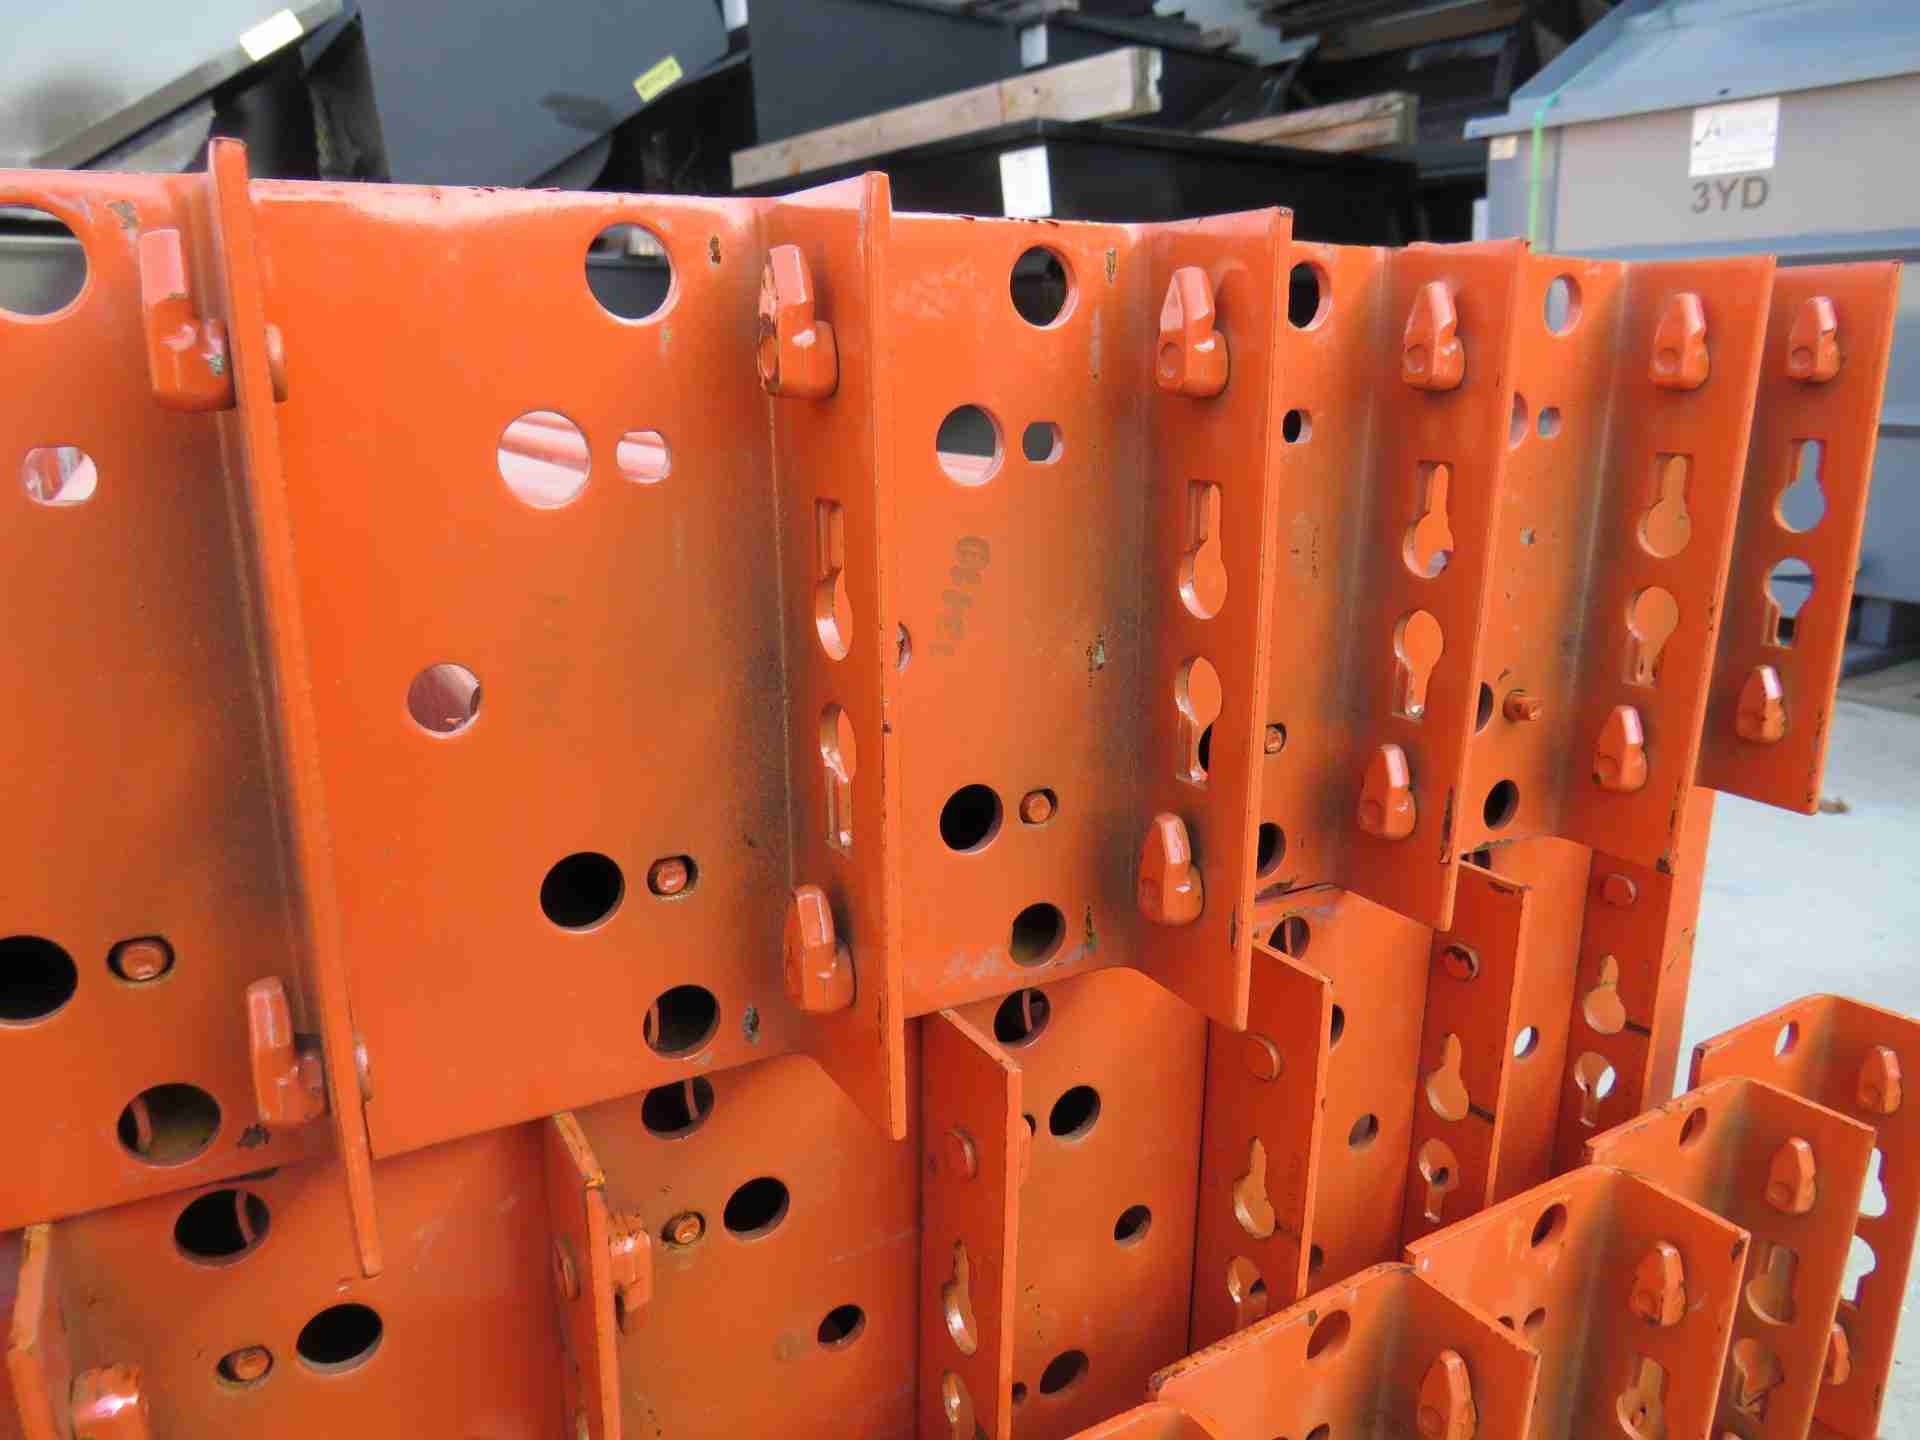
How Does Pallet Racking Support Regulatory Compliance?
Can Pallet Racking Reduce Contamination Risks?
Look, anyone who’s spent time in a warehouse or a workshop knows dirt and grime have a sneaky way of creeping in where you don’t want them. When it comes to handling goods, especially in food, medical, or cleanroom settings, contamination isn’t just a nuisance—it’s a real threat. That’s where pallet racking steps up not just as shelving, but a frontline defender of cleanliness.
Pallet racking puts order into chaos. By lifting products off the floor and stacking them neatly, it stops dust bunnies from setting up camp under crates, and it keeps forklifts from dragging dirt straight onto your inventory. This simple, sturdy setup creates barriers—not walls, but spaces that let you clean the floor properly and regularly without moving entire stacks. It’s the difference between a place that’s “clean enough” and one that meets strict contamination standards.
There’s something satisfying about the pragmatism of it all. Pallet racking isn’t fancy; it’s built tough and designed to make your life easier. When you install a solid pallet racking system, you are investing in routine and discipline because it demands a methodical approach. You arrange your goods, keep pathways clear, and you’re forced to keep tabs on what’s coming in and out. This reduces the chance of cross-contamination because everything’s not just dumped in the same pile or running across the floor. You’re managing inventory in a way that respects safety and health, without turning your workspace into a maze of hazards.
From a moral standpoint, if you’re dealing with products that people consume or depend on, you owe it to them—and to yourself—to keep those goods safe. Pallet racking is one of those quietly effective tools that say, “We care enough to do things right.” It’s not just about meeting regulations; it’s about the pride in knowing you’re part of a process that protects workers, customers, and communities.
At the end of the day, pallet racking is a no-nonsense way to take control. It’s about rolling up your sleeves, setting a standard, and having confidence that your space supports the health and safety everyone deserves. When you see those rows of pallets neatly organized, it’s not just storage—it’s trust built on steel and sweat.

Can Pallet Racking Reduce Contamination Risks?
Can Pallet Racking Reduce Contamination Risks?
- Dirt and grime pose serious contamination risks in food, medical, and cleanroom settings.
- Pallet racking elevates goods off the floor, preventing dust accumulation and dirt transfer from forklifts.
- The design allows regular floor cleaning without moving entire inventory stacks, maintaining strict cleanliness standards.
- Pallet racking encourages routine, discipline, and organized inventory management, reducing cross-contamination.
- It promotes safety and health by keeping pathways clear and preventing unsafe clutter.
- Using pallet racking reflects a commitment to product safety, regulatory compliance, and protecting workers and communities.
- Neatly organized pallet racks symbolize control, standard-setting, and trust in maintaining a clean, safe workspace.

Can Pallet Racking Reduce Contamination Risks?
How Does Optimized Pallet Racking Save Operational Costs?
Look, anyone who’s spent time in a warehouse knows the chaos of cluttered aisles and stacks of pallets piled high like they’re about to cave in. Pallet racking that’s tuned right doesn’t just make the space look sharp—it’s like giving your whole operation a shot of adrenaline. When your racks are set up to move pallets smoothly and safely, you’re cutting down the time folks spend hunting for stuff or juggling loads. Less time wasted means more orders filled, and that’s money back in your pocket at the end of the day.
But it’s not just about hustling faster. Optimized pallet racking means fewer accidents, which is a real win for everyone involved. Broken pallets, smashed goods, or, worse, injuries—that’s a cost no one wants to carry. When racks are sturdy and arranged with real thought, it shows you care about the hands doing the work and the product you’re handling. That kind of responsibility builds trust not just among your crew but with clients who know their shipments won’t show up looking like a shipping disaster.
From a numbers point of view, smart pallet racking saves cash in ways you might not expect. You can stack more without risking a heap of boxes tumbling like dominoes. It frees up floor space so you can squeeze in more inventory, meaning fewer rush orders or emergency shipments. Saving on storage rental or expanding onto new warehouse space? That cost adds up fast, and well-planned racks keep you from reaching for that checkbook too soon.
Think about it like this: your warehouse is a machine, and pallet racking is the backbone holding everything steady. When it’s optimized, it runs smoother, safer, and cheaper. Everyone from the forklift drivers maneuvering through tight aisles to the managers keeping the books feels the difference. It’s humble, honest work but setting it right pays off big, every time. So don’t just throw up any racking and call it done—put in the effort, and watch how it makes your operation leaner, safer, and smarter. That’s cost-saving done the right way.

How Does Optimized Pallet Racking Save Operational Costs?
How Does Optimized Pallet Racking Save Operational Costs?
- Optimized pallet racking improves warehouse efficiency by enabling smooth, safe pallet movement, reducing time spent searching or handling loads.
- Efficient rack setup increases order fulfillment speed, directly boosting profitability.
- Well-arranged, sturdy racks reduce accidents, protecting workers and inventory from damage and injury.
- Thoughtful pallet racking builds trust among employees and clients by ensuring safe, reliable shipment handling.
- Smart racking maximizes stacking capacity and frees floor space, allowing more inventory storage and fewer emergency shipments.
- Effective pallet racking lowers costs by minimizing the need for additional storage rental or warehouse expansion.
- Optimized racks stabilize warehouse operations, benefiting everyone from forklift drivers to managers and enhancing overall safety and cost savings.

How Does Optimized Pallet Racking Save Operational Costs?
Conclusion
Pallet racking in drug manufacturing facilities is the unsung hero that keeps the whole operation steady, safe, and on schedule. It’s not just about putting boxes on shelves—it’s about respect for the work, the product, and the lives depending on those medicines. A well-built racking system transforms chaos into calm, turning cramped storage into a streamlined flow where every pallet has its place, easy to find and safe from harm. This kind of order isn’t just good housekeeping; it’s a lifeline. When everything’s organized right, wasted time and costly mistakes get knocked down, and the job of delivering vital drugs gets done right every time.
Behind every pallet lies a story of sweat and responsibility, and pallet racking carries that weight without flinching. It keeps products off the floor, away from dirt and damage, securing them like a fortress built on years of trial and error. When inspectors come by, these racks tell a story of compliance and care, a silent guarantee that the company values safety, integrity, and the trust of the people relying on their medicines. It’s a tough, practical setup that fits just right in tight spaces and is flexible enough to roll with the punches of changing needs.
More than just metal beams, pallet racking is the backbone of quality control. It holds everything steady, preventing mix-ups and damage that could erode trust and cost lives. It’s the quiet enforcer of good habits, making audits and inspections smoother and signalling to workers and customers alike that this place takes its standards seriously. That peace of mind—that products are handled properly and delivered intact—doesn’t come from fancy packaging, but from solid, commonsense storage.
Running a drug manufacturing facility means playing by the rules, and pallet racking is a frontline player in staying compliant with tough regulations. Properly installed racks keep weight limits, spacing, and fire codes in check, preventing costly fines and dangerous accidents. That’s not just ticking boxes—it’s doing right by employees, customers, and the community. A warehouse that meets these standards doesn’t just survive inspections; it earns respect.
Then there’s contamination risk—something nobody wants lurking around medicines. Pallet racking helps keep the dirt out by raising goods off the floor and letting crews clean without hassle. This simple, rugged solution reflects a daily commitment to doing things right: protecting products, people, and the wider community alike.
Finally, optimized pallet racking saves hard-earned cash. It cuts down on wasted time, reduces accidents, and maximizes storage space so fewer emergency orders clog up the works. It’s like giving your operation a reliable backbone that keeps everything moving smooth, safe, and smart. When you set up your racks right, you’re not just stacking pallets—you’re stacking trust, safety, and respect. That’s the kind of no-nonsense solution that holds a drug manufacturing facility upright, day in and day out.

Conclusion
Conclusion:
- Pallet racking in drug manufacturing facilities organizes storage efficiently, ensuring safety and timely operations.
- It protects products from dirt and damage by keeping them off the floor, supporting compliance and trust.
- Racking systems prevent mix-ups and damage, aiding quality control and facilitating audits and inspections.
- Proper installation ensures compliance with regulations, including weight limits, spacing, and fire codes.
- Pallet racks reduce contamination risk by enabling easy cleaning and maintaining product integrity.
- Optimized racking saves time, reduces accidents, and maximizes storage space, enhancing operational efficiency.
- Overall, pallet racking supports trust, safety, and respect, forming the backbone of steady drug manufacturing operations.

Conclusion
Other Resources

Other Resources
Here is a list of other resources you can review online to learn more:
- Pallet Racking systems in Illinois and Great Lakes
- RMI
- Teardrop Uprights
- Storage Equipment Manufacturers Association
- Interlake Mecalux
- CMMA
- Interlake
- CA Wire
- Illinois Pallet Racking – Storage Solutions
- Material Handling Safety
- BMH
- Warehouse Storage Racks
- Cantilever Rack Guide: Ordering Cantilever Racking
- Teardrop Pallet Rack – Ridg-U-Rak
- Material Handling Industry
- IWLA
- Used Teardrop Pallet Rack – American Surplus
- IIWS Inc. Rack Installation Illinois & Rack Repairs Illinois
- Warehouse Racking Systems: Beginner’s Guide to Rack Systems
Use This Prompt To Get More Resources With Your Favorite Online AI Tool: Please provide me with a list of online articles with their URLs in a bulleted list that I can read regarding How Do Drug Manufacturing Facilities Leverage Pallet Racking?

Other Resources
Glossary Terms
How Do Drug Manufacturing Facilities Leverage Pallet Racking? – Glossary Of Terms
1. Pallet Racking: A storage system designed to hold materials on pallets in horizontal rows with multiple levels.
2. Warehousing: The process of storing goods in a dedicated facility.
3. Inventory Management: Techniques used to oversee and control stock levels.
4. Space Optimization: Maximizing use of available storage area.
5. Load Capacity: The maximum weight a pallet rack can safely hold.
6. Safety Compliance: Adherence to laws and regulations governing safe storage practices.
7. Material Handling: The movement, protection, storage, and control of materials.
8. Accessibility: Ease of reaching and retrieving stored items.
9. FIFO (First In First Out): Inventory rotation method ensuring the oldest stock is used first.
10. LIFO (Last In First Out): Inventory rotation method where the most recently stored items are used first.
11. Structural Integrity: The rack system’s ability to maintain stability under load.
12. Adjustable Beams: Horizontal components that can be repositioned to accommodate different pallet heights.
13. Selective Racking: A basic form of pallet racking allowing direct access to each pallet.
14. Drive-In Racking: A system allowing forklifts to drive directly into the rack’s lanes.
15. Push Back Racking: A system where pallets are stored on nested carts that move along inclined rails.
16. Pallet Dimensions: The standardized size of pallets used in storage.
17. Forklift Compatibility: The ability of storage systems to accommodate forklift operations.
18. Load Distribution: Even spreading of weight across pallet racks.
19. Rack Protection: Accessories like guards and barriers preventing damage.
20. Modular Design: A system constructed with interchangeable components.
21. Vertical Storage: Utilizing height for additional storage capacity.
22. Pharmaceutical Grade Storage: Storage conditions compliant with drug manufacturing standards.
23. Environmental Controls: Systems managing temperature, humidity, and cleanliness.
24. Inventory Traceability: The ability to track the location and movement of stock.
25. Lean Warehousing: Minimizing waste and inefficiencies in storage processes.
26. Ergonomics: Designing processes to improve worker comfort and productivity.
27. Cleanroom Compatibility: Suitability for environments with strict contamination controls.
28. Real-time Inventory: Up-to-date information on stock status.
29. Automation Integration: Incorporating automated systems with pallet racking.
30. Regulatory Standards: Official requirements governing storage in drug manufacturing.

Glossary Of Terms
Other Questions
How Do Drug Manufacturing Facilities Leverage Pallet Racking? – Other Questions
If you wish to explore and discover more, consider looking for answers to these questions:
- What types of pallet racking systems (selective, drive-in, push-back, pallet flow, cantilever, etc.) are best suited for different pharmaceutical storage needs?
- How do you determine required load capacities and safety factors for each rack line?
- What racking designs support strict FIFO (first-in, first-out) or FEFO (first-expire-first-out) inventory rotation?
- How do pallet racking choices affect cold chain and temperature-controlled storage?
- What materials and finishes (galvanized, powder-coated, stainless steel) are recommended to prevent corrosion and contamination?
- How should pallet racking be configured to minimize contamination and cross-contamination risks?
- What cleaning and sanitization protocols apply to racking in GMP/cleanroom-adjacent areas?
- How can racking support segregation of high-potency, hazardous, or controlled substances?
- What are the applicable regulatory and industry standards (FDA, cGMP, OSHA, NFPA, ISO) for pallet racking in pharma facilities?
- What documentation and records related to racking (installation, inspections, maintenance, load tests) auditors expect to see?
- How often should racking be inspected and what should routine inspection checklists include?
- What are best practices for rack maintenance, repair, and replacement of damaged components?
- How do fire protection systems (sprinkler layout, clearances, fire codes) interact with rack design?
- What seismic bracing, anchoring, or anti-collapse measures are required in earthquake-prone regions?
- How do floor loading limits and concrete strength influence rack placement and aisle layout?
- What aisle widths and clearances are needed for safe forklift operation and regulatory compliance?
- Which pallet types and formats (stringer, block, plastic, heat-treated) are compatible with different racking systems?
- How can pallet racking integrate with WMS/ERP systems for lot tracking, serialization, and automated picking?
- What options exist for adding sensors, temperature/humidity monitors, or load-monitoring devices to racks?
- How do automated storage and retrieval systems (AS/RS), conveyors, and robotics integrate with pallet racking?
- What are the cost factors and expected ROI when upgrading or optimizing pallet racking?
- How much downtime or operational disruption should be expected during installation or retrofit, and how can it be minimized?
- What training and certification programs are needed for staff to work safely with pallet racking and lift equipment?
- How should racking be designed to support efficient picking workflows and worker ergonomics?
- What measures reduce damage during handling (pallet protectors, column guards, rack end protectors)?
- How do you plan for scalability and future changes in product mix, packaging, or storage volume?
- What are the pros and cons of modular or movable racking systems versus fixed installations?
- How is racking performance measured (KPIs like picking time, space utilization, damage rates) after optimization?
- What contingency plans and procedures exist for product recalls, quarantines, or rapid removal from racks?
- How do racking layouts affect HVAC airflow, cleanroom classifications, and environmental monitoring?
- What pest control and hygiene strategies are compatible with racking designs?
- How do insurance requirements and premiums relate to racking condition and compliance?
- What warranty, service, and spare-parts options should be negotiated with racking suppliers?
- How are racking installations validated and qualified for GMP/regulatory inspections?
- What testing or load-certification is recommended before putting racks into service?
- How should hazardous materials labeling, signage, and access-controls be implemented on racking?
- What sustainability and recyclability considerations apply to rack selection and end-of-life disposal?
- Are there case studies or benchmarks showing measurable benefits from specific racking upgrades in pharma facilities?

Other Questions
Checklist
How Do Drug Manufacturing Facilities Leverage Pallet Racking? – A Checklist
Planning and Layout
✅______ Facility zoning defined for raw materials, WIP, finished goods, quarantine, and rejected materials
✅______ Flow paths designed for unidirectional material movement to prevent mix-ups
✅______ Aisle widths matched to material handling equipment turning radii and clearance needs
✅______ Dedicated receiving, sampling, and release areas identified and separated
✅______ Strategic locations for high-velocity SKUs placed for minimal travel time
✅______ Clear location numbering schema established (aisle–bay–level–position)
Rack Design and Engineering
✅______ Racks engineered to applicable codes (RMI/ANSI MH16.1 and local building and seismic)
✅______ Load calculations documented, including pallet, product, and dynamic loads
✅______ Load capacity signage posted at aisle ends and per bay
✅______ Proper anchoring and seismic bracing installed as required
✅______ Beam locking pins and safety clips installed on every beam
✅______ Column protectors and end-of-aisle guards installed
✅______ Decking type selected for use case (wire mesh, solid, or slatted) with load ratings
✅______ Pallet overhang and beam spacing validated for pallet type and size
✅______ Flue spaces designed (longitudinal and transverse) and marked to maintain sprinkler performance
Fire Protection and Egress
✅______ Rack layout coordinated with sprinkler design and hazard classification
✅______ Minimum distances maintained from sprinklers and ceilings per code
✅______ In-rack sprinklers used where required by commodity class and configuration
✅______ Aisles and exits unobstructed; egress routes clearly marked
✅______ No shrink-wrap, slip sheets, or debris blocking flue spaces
✅______ Fire extinguishers, alarms, and signage accessible and visible
Pallets and Containers
✅______ Approved pallet types defined by area (e.g., plastic for clean zones; no broken wood)
✅______ Pallet condition inspection criteria in place (no cracks, protruding nails, contamination)
✅______ Standardized pallet dimensions and weights documented
✅______ Compatible totes, bins, and containment selected for APIs and hazardous materials
Inventory Control and Traceability
✅______ FEFO/FIFO rules defined and enforced via location strategy
✅______ Barcoding or RFID enabled at pallet and case level (lot, batch, expiry)
✅______ WMS locations mapped to rack addresses with scan verification
✅______ Quarantine and released status controlled by system, not label alone
✅______ Cycle counting program aligned to risk and value (ABC)
✅______ Physical and system counts reconciled with deviation handling
Quality and cGMP Compliance
✅______ SOPs cover racking use, loading, unloading, and housekeeping
✅______ Line clearance and segregation procedures documented and enforced
✅______ Change control required for any rack reconfiguration or capacity change
✅______ Deviations, damage, or spills recorded with CAPA where applicable
✅______ Vendor documentation retained for rack design, installation, and certification
✅______ Audit trail available for storage, moves, and releases
Contamination Control
✅______ Materials stored off the floor; lowest beam height allows floor cleaning
✅______ Wire mesh or solid decking selected to minimize product fall-through where needed
✅______ Drip pans or containment used under spill-risk items (liquids, solvents)
✅______ Dust control measures in place; overhead dust sources mitigated
✅______ Area-specific cleaning schedules established for racks and aisles
✅______ Allergen, sensitizer, and potent compound segregation validated
✅______ Pest control access and inspection points unobstructed
Environmental Controls
✅______ Racks do not obstruct airflow in temperature- or humidity-controlled rooms
✅______ Temperature and RH mapping completed with probes at representative rack locations
✅______ Continuous monitoring with calibrated sensors and alarm thresholds
✅______ Procedures for excursions, quarantine, and product impact assessment
✅______ Corrosion-resistant finishes used where required (cold rooms, clean areas)
Safety and Ergonomics
✅______ Safe lifting heights established; no manual picks above ergonomic limits
✅______ Fall protection in place for elevated work (mezzanines, pick modules)
✅______ Forklift clearances marked; rack end guards protect traffic lanes
✅______ Traffic management plan includes speed limits and right-of-way
✅______ Signage for maximum pallet stack heights and safe handling posted
✅______ Adequate lighting levels maintained for picking and inspection
Operations and Training
✅______ Operators trained and certified on equipment and rack-specific SOPs
✅______ Visual aids posted (load charts, location maps, FEFO rules, cleaning steps)
✅______ Standard work for receiving, put-away, replenishment, and picking
✅______ Incident and near-miss reporting encouraged and reviewed
✅______ Contractors and visitors briefed on rack safety rules
Inspection and Maintenance
✅______ Routine rack inspections scheduled (daily visual, monthly detailed, annual professional)
✅______ Damage criteria defined (deflection, dents, bent uprights) with immediate tag-out
✅______ Preventive maintenance for anchors, beams, decking, and guards
✅______ Pallet inspection at receipt and before racking
✅______ Documented repairs by qualified personnel; records retained
✅______ Flue space audits conducted and corrected promptly
Security and Controlled Substances
✅______ Secure cages or vaults for controlled substances with restricted access
✅______ Access control and CCTV coverage for high-risk zones
✅______ Segregated storage for hazardous, flammable, or temperature-sensitive goods
✅______ Chain-of-custody procedures enforced for controlled materials
Cost and Space Optimization
✅______ Vertical cube fully utilized within safe and code-compliant limits
✅______ Slotting analysis performed to reduce travel and touches
✅______ Dynamic vs. static storage matched to demand profile (drive-in, pushback, flow)
✅______ Modular rack components selected for future reconfiguration
✅______ KPI dashboard tracks picks/hour, damage rate, space utilization, and OTIF
✅______ Lean 5S applied to aisles, end caps, and staging zones
Readiness and Continuous Improvement
✅______ Pre-go-live validation completed (walk-through, mock picks, and stress tests)
✅______ Post-implementation review conducted with corrective actions
✅______ Periodic re-slotting and capacity review aligned to demand changes
✅______ Lessons learned captured; SOPs and training updated accordingly

Checklist
At RackingWorld, we help guide you through selecting warehouse storage systems and racking.
Be sure to read our other related stories at RackingWorld to learn more about warehouse storage systems.
0 Comments